Pump impeller balancing corrects the distribution of mass around the rotation axis so that residual unbalance meets the agreed requirement. A useful balance report identifies exactly what was tested, how it was mounted, which correction planes were used and what residual unbalance remained. It does not prove that the installed pump is aligned, hydraulically suitable or free from every cause of vibration. Before ordering balancing work, define the impeller or rotor assembly, operating speed, permitted correction method and acceptance basis with the equipment manufacturer and repair specialist.
This guide helps industrial water-pump owners write a repair scope and review the resulting evidence. It is not an instruction for grinding an impeller or running an exposed rotor. Balance-machine operation, material removal and rotor repair belong to qualified personnel working to an approved procedure.
Separate mass balance from hydraulic performance
Mass unbalance describes how mass is distributed around the rotation axis. Hydraulic performance concerns how the pump transfers energy to the liquid. A rotor can meet a balance requirement and still operate poorly because of an unsuitable duty point, damaged passages, incorrect clearances, air entry or another hydraulic problem.
Likewise, vibration measured on an installed pump has several possible causes. Do not order material removal solely because one vibration amplitude is high. Record speed, operating flow, bearing condition, alignment and the recent repair history before deciding which inspection is needed. Our pump vibration measurement guide describes the operating baseline that makes these comparisons useful.
For procurement, keep hydraulic acceptance and mechanical balance acceptance separate in the repair specification. Each needs evidence appropriate to its purpose; a balance certificate cannot replace a pump performance test.
Identify the exact component and service condition
Record the pump model, serial identification, impeller marking, actual diameter, material and operating speed range. Photograph the component before cleaning and after inspection. If the original marking is missing, resolve identification with drawings and measured dimensions rather than assigning a model from appearance alone.
State whether the work concerns a loose impeller, an impeller on its shaft, a rotor containing multiple stages, or another defined assembly. Include keys, sleeves, nuts and other rotating parts according to the applicable balancing convention. The condition represented by the test should be clear enough for the assembly technician to reproduce.
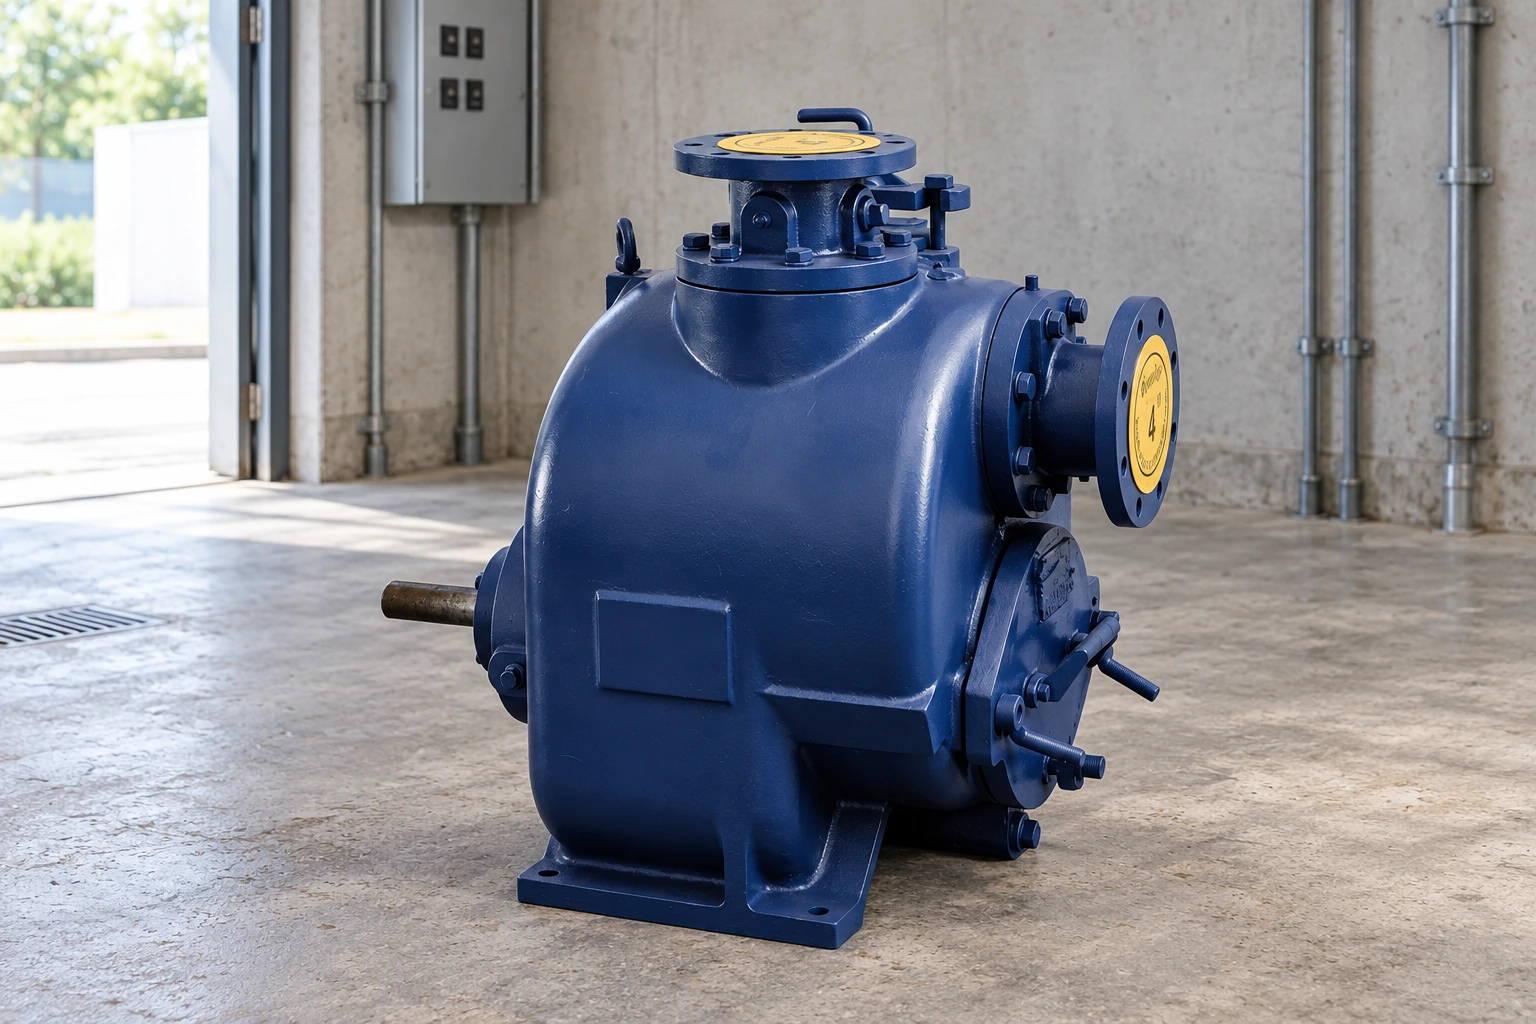
A pump family page such as the IS clean-water centrifugal pump range establishes relevant equipment context. It does not establish a balance grade, rotor construction or machining allowance for every size. Obtain the specific manufacturer’s documents for the delivered unit.
Inspect damage before asking the balancing machine to correct it
Clean the component using an approved process and inspect for deposits, corrosion, erosion, cracks and previous repair. Material build-up may change mass distribution, while uneven wear can also damage hydraulic surfaces. Preserve photographs and findings before altering the evidence.
An impeller that is cracked, badly thinned or dimensionally unacceptable needs an engineering disposition. Balancing cannot restore strength or recreate missing hydraulic geometry. Similarly, applying a coating or making a weld repair may change both mass and suitability for service; the repair method must be approved before the final balance check.
Наш centrifugal pump impeller types guide explains why an open, channel or other impeller cannot be treated as an interchangeable shape. Correction locations must respect the actual component design and its permitted repair limits.
Understand what static and dynamic evidence can show
A static check can reveal a heavy side under appropriate conditions. Dynamic balancing evaluates behavior in rotation and may be performed using one or more correction planes, depending on the rotor and the agreed method. The number of planes should be selected from the geometry, support arrangement and specification, rather than from a blanket rule that every pump needs the same process.
An overhung impeller presents a different arrangement from a long rotor supported between bearings. Ask the repair specialist how the chosen setup represents the actual component and how fixture effects are controlled. A component passing an informal static check does not automatically satisfy a specified dynamic balancing requirement.
EASA’s discussion of dynamic balancing on pump impellers notes the importance of pump rotor geometry. Use the applicable standard and manufacturer’s requirement for the actual job; this article does not assign a universal balance quality grade.
Agree the acceptance basis before the repair starts
The repair order should identify the governing document and revision, the balancing speed or approved method, units, correction planes and the definition of the accepted residual unbalance. Clarify whether a limit applies to the complete component or is allocated between planes. Ambiguity here can produce two apparently valid certificates describing different acceptance conditions.
If an ISO balance grade is specified, the associated speed and rotor data matter. A grade name alone is not a complete shop instruction. The owner should have the specialist document how the requirement is converted into the applicable residual-unbalance limit for this component.
Avoid copying a grade from an unrelated pump purchase specification. A more stringent number is not automatically useful if the measurement setup, component condition or repair process cannot substantiate it. Resolve the specification before material is removed.
Control mounting, fixtures and measurement repeatability
The shaft, arbor, adaptor and locating surfaces used during balancing can influence the result. Inspect fits and cleanliness and document how the component is located. A worn or eccentric mounting arrangement can create a misleading response even when the impeller itself has been corrected carefully.
Specify the key convention and identify the rotating hardware included in the setup. The repairer should be able to explain how those choices correspond to the final assembled condition. Where the agreed procedure requires repeat mounting or another verification, keep that evidence with the report.
Do not confuse geometric runout with mass unbalance. A component may need dimensional inspection as well as balancing. Our centrifugal pump runout guide addresses a complementary measurement question: whether the rotating geometry is true to the intended reference.
Review the work through clear hold points
The table below is a repair-scope checklist. It does not prescribe a machining method or numerical limit.
| Hold point | Доказательства для запроса | Reason to pause the work |
|---|---|---|
| Component identification | Marking, dimensions and assembly drawing | Component or material cannot be confirmed |
| Condition inspection | Cleaning record, damage photographs and disposition | Strength or geometry is unacceptable |
| Balance setup | Mounting arrangement, included hardware and key convention | Fixture or assembly condition is unclear |
| Correction authorization | Approved locations and repair method | Proposed removal affects prohibited areas |
| Final acceptance | Before-and-after values, units and applied limits | Report omits the acceptance calculation or component identity |
| Reassembly | Orientation, fits, fasteners and inspection record | Accepted balance condition cannot be reproduced |
Make each hold point an actual decision in the repair order. A checklist completed after the pump has been shipped gives the owner less opportunity to resolve uncertainty.
Treat trimming and other modifications as separate approvals
Changing impeller diameter is a hydraulic modification as well as a physical change to a rotating component. The need for a subsequent balance check should be included in the approved modification scope. Do not treat balancing as authorization to alter the diameter, blade profile or passage geometry.
If the proposed repair includes trimming, review the duty requirement, performance implications and manufacturer’s permitted limits through the impeller trimming guide. Keep the final diameter and drawing revision on the balance report so that future inspections refer to the actual repaired condition.
The same principle applies after coating, weld repair or replacement of rotating hardware. Define the final condition before the acceptance check. A certificate for the previous configuration may no longer represent the assembly returned to service.
Read the certificate as a traceable measurement record
A useful certificate should identify the customer equipment, component, date, operator or responsible organization, machine or setup, measurement units, test arrangement and acceptance basis. Request initial and final results in an understandable form, with residual values and limits clearly associated with the relevant planes or assembly.
Check that the document names the component actually returned. Confirm the dimensions and configuration against the repair order. If the report states only “balanced OK,” ask for the missing measurement information before accepting it as proof of a specified requirement.
Where a report includes a balance grade, ensure that its supporting speed and mass assumptions match the agreed scope. Unexplained differences should be resolved with the repair specialist, not interpreted by guessing which number is more conservative.
Reassemble without losing the accepted condition
Follow the manufacturer’s instructions for shaft fits, key installation, orientation, retaining hardware and tightening. Protect locating surfaces from damage and contamination. Parts that were balanced as an assembly need the defined relationship preserved during reassembly, or an approved explanation of why a different relationship remains acceptable.
Complete the separate checks for clearances, free movement, lubrication, sealing and alignment. EPRI’s vertical pump maintenance and repair guidance illustrates that rotor balance belongs within a broader repair process. Its pump-specific examples are not universal limits for horizontal water pumps.
After authorized startup, compare operating measurements against a suitable baseline. If vibration remains high, investigate the operating and installation condition. Do not immediately ask for another balance correction without considering the evidence from the complete assembly.
Повышение квалификации
The NPTEL rotor-balancing lecture below explains the mechanical principles behind balancing a rigid rotor. It supports understanding of mass distribution and correction, but does not replace a pump manufacturer’s repair instruction or authorize field trial weights on operating machinery.
Часто задаваемые вопросы
Does a balanced impeller guarantee a vibration-free pump?
No. Installed vibration can also involve alignment, bearings, supports, hydraulic conditions and other faults. A balance report addresses the defined component and test condition, so operational verification remains necessary.
Is static balancing sufficient for every impeller?
No. The required method depends on the component geometry, assembly arrangement and agreed specification. Ask the manufacturer and repair specialist to identify the appropriate method and acceptance evidence.
Can balancing repair a corroded or cracked impeller?
It cannot restore lost strength or unacceptable geometry. Inspect and approve the component condition first. Repair or replacement must be decided before the final balance acceptance step.
Should an impeller be checked after trimming?
Include the required balance verification in the approved trimming scope. The final component configuration must be the one represented by the acceptance report, subject to the manufacturer’s instructions.
What is the minimum useful balance report?
It should identify the actual component, mounting and included hardware, method, units, governing requirement, initial condition and final residual results. A brief pass statement without these details may not demonstrate the specified acceptance requirement.