Pump casing alignment register inspection checks the locating surfaces that position stationary components relative to one another. Identify the mating registers, clean and examine them, measure the specified diameters and verify the required relationship to the equipment’s reference centerline. A joint can bolt together and seal while its locating features remain damaged or incorrectly aligned. Inspection therefore needs the drawing, defined datums and measurements of both mating parts. Bolt-hole alignment and a visually even joint are useful observations, but they do not prove that the internal stationary geometry meets the design.
This guide addresses register inspection during an industrial pump overhaul. It is separate from coupling alignment and from the inspection of a casing gasket face. The exact register arrangement, allowable fit and geometric requirements depend on the pump construction; no universal clearance or runout limit is supplied here.
Distinguish a locating register from a sealing face
A register is a locating feature, often a mating cylindrical diameter or step. A nearby face may perform a sealing or axial locating function, and the two features can affect the same assembly. Identify them individually on the sectional drawing. Record which component contains the male feature, which contains the female feature and which surfaces establish the reference geometry for inspection.
Do not assume that every machined circular edge is the intended register. A relief, gasket recess or clearance feature can look similar when viewed on a dismantled part. Trace the drawing callouts and original part numbers before measurement. If the original drawing is unavailable, document the observed geometry and request clarification before authorizing machining or declaring the fit acceptable.
Understand why local dimensions and alignment both matter
Das EPRI Wartungsleitfaden für Vertikalpumpen explains the relationship between stationary-component registers and the common centerline of bearings and wear rings. Its discussion concerns vertical pump construction and must be applied within that scope. The useful inspection principle is to examine the geometry of the connected components, rather than assuming that external motor alignment corrects an internal locating defect.
A measured diameter describes size at a location. It does not by itself establish the relationship of that diameter to another bore or face. Conversely, an apparently concentric setup does not show that the mating fit has the required size. Plan the size checks and geometric checks as distinct tasks, using the datums and methods specified for the actual pump.
Preserve assembly identity before separating components
Record the equipment tag, model, serial number and drawing revision. Photograph the joint and identify the matching components and their original orientation. Where several bowls, casings or adapters are present, maintain an ordered parts map. Mixing two similar components can make an inspection record unusable even when each individual measurement was taken accurately.
Apply the site’s isolation, draining and safe lifting procedures before disassembly. Consider trapped pressure, process residues and unsupported component weight. The HSE-Wartungsrichtlinien describes general precautions; the pump’s approved procedure governs the particular intervention. Do not use joint bolts to force apart an arrangement that requires designated jacking points or a specific handling sequence.
Examine the as-found register before cleaning
Photograph corrosion, fretting-like marks, displaced material and evidence of uneven contact. Identify the position and width of significant marks relative to the parts map. Keep deposits for examination when they may help explain a loss of fit or unusual wear. Distinguish a raised burr from an area where material has been lost, because each can affect the assembled condition differently.
Choose cleaning methods that preserve the machined surfaces. Remove loose contamination without rounding an edge or changing the locating diameter. Heavy abrasion can make a component look cleaner while destroying the feature being inspected. If dressing or machining is authorized, record the original condition first and treat the work as a repair with its own dimensional verification.
Plan the measurements around defined datums
List the required measurements before setting up the part. Identify the male and female register diameters, relevant face condition and the reference feature for any concentricity or perpendicularity check. Include the measurement method and instrument capability in the inspection plan. A convenient exterior surface should not become a datum merely because it is easy to grip or indicate.
Record readings at the positions required by the approved method. Multiple angular and axial locations may be needed to describe form; the actual procedure should define them. Keep the individual readings rather than reporting only a mean. An average can hide a local high point or a directional difference that affects assembly. State whether an indicated reading is a diameter, a radial displacement or total indicated movement.
Control the measurement setup carefully. Dirt, unstable support or an unsuitable reference can produce misleading results. Record instrument identification and the setup arrangement, and verify repeatability when the measurement affects repair acceptance. If the uncertainty is too large to support a decision, improve the method or request a competent metrology review instead of rounding the reading into tolerance.
Use a register-specific inspection sheet
The following qualitative table organizes the work. It does not prescribe allowable clearance, geometric tolerance or machining stock. Add the actual acceptance requirement and drawing reference to each applicable row.
| Feature or task | Aufzubewahrende Beweismittel | Question it helps answer |
|---|---|---|
| Mating-part identity | Part numbers, orientation and assembly map | Are the intended components being compared? |
| Register surface | Photographs of raised material, wear and corrosion | Could damage disturb location or seating? |
| Male and female size | Individual readings, units and positions | Does the actual mating fit meet its specification? |
| Reference geometry | Datum, setup and indicated results | Is the locating feature related correctly to the required centerline? |
| Joint face | Condition and specified geometric checks | Can the assembly seat as designed? |
| Repaired feature | Authorized work and final dimensions | Has the repair restored the required geometry? |
| Assembly verification | Joint condition and required movement checks | Are the inspected parts assembled without unresolved interference? |
Keep the report’s observation and disposition fields separate. A statement such as “localized raised material on the register edge” records a finding. Whether the part needs cleaning, approved dressing, machining or replacement is a decision based on the actual requirement. Keeping both fields prevents a conclusion from replacing the evidence needed to review it.
Recognize the limits of trial assembly
A trial assembly can reveal an obvious interference or an incorrectly matched component. It cannot replace the required dimensional inspection. A joint drawn together by bolts may conceal a locating problem, and a part that enters easily may have excessive clearance. Do not tighten bolts to overcome unexplained resistance or assume that the resulting joint proves the register acceptable.
Use the specified assembly conditions, including the correct gasket or other joint arrangement where applicable. A measurement taken on a loose stack may not represent the final condition. Record what was fitted and what remained absent during each check. If the procedure requires verification before an inaccessible joint is closed, establish a hold point and retain the findings before continuing.
Define repair scope before changing a locating surface
A repair proposal should identify the defective feature, its relationship to the adjoining components and the geometry that must be restored. Machining a single diameter without considering its reference centerline or adjacent face can leave the assembly with another unresolved error. Have the responsible engineer or supplier approve the repair method and the final inspection requirements.
After repair, remeasure the affected features and the relevant mating parts. Keep the original and final records together. Do not use a generic register clearance, a tolerance from a different pump or an undocumented workshop rule as the release criterion. When the design requirement cannot be confirmed, retain the part in a controlled review state and provide the measurements to the decision maker.
Connect the findings to the wider overhaul
Register inspection complements the casing flange-face examination but does not replace it. A sealing face and a locating diameter address different aspects of the joint. It also complements the Pumpenwellen-Ausrichtungsmethoden used later in the maintenance process. External alignment should follow confirmation that the internal assembly has been repaired and assembled to its own requirements.
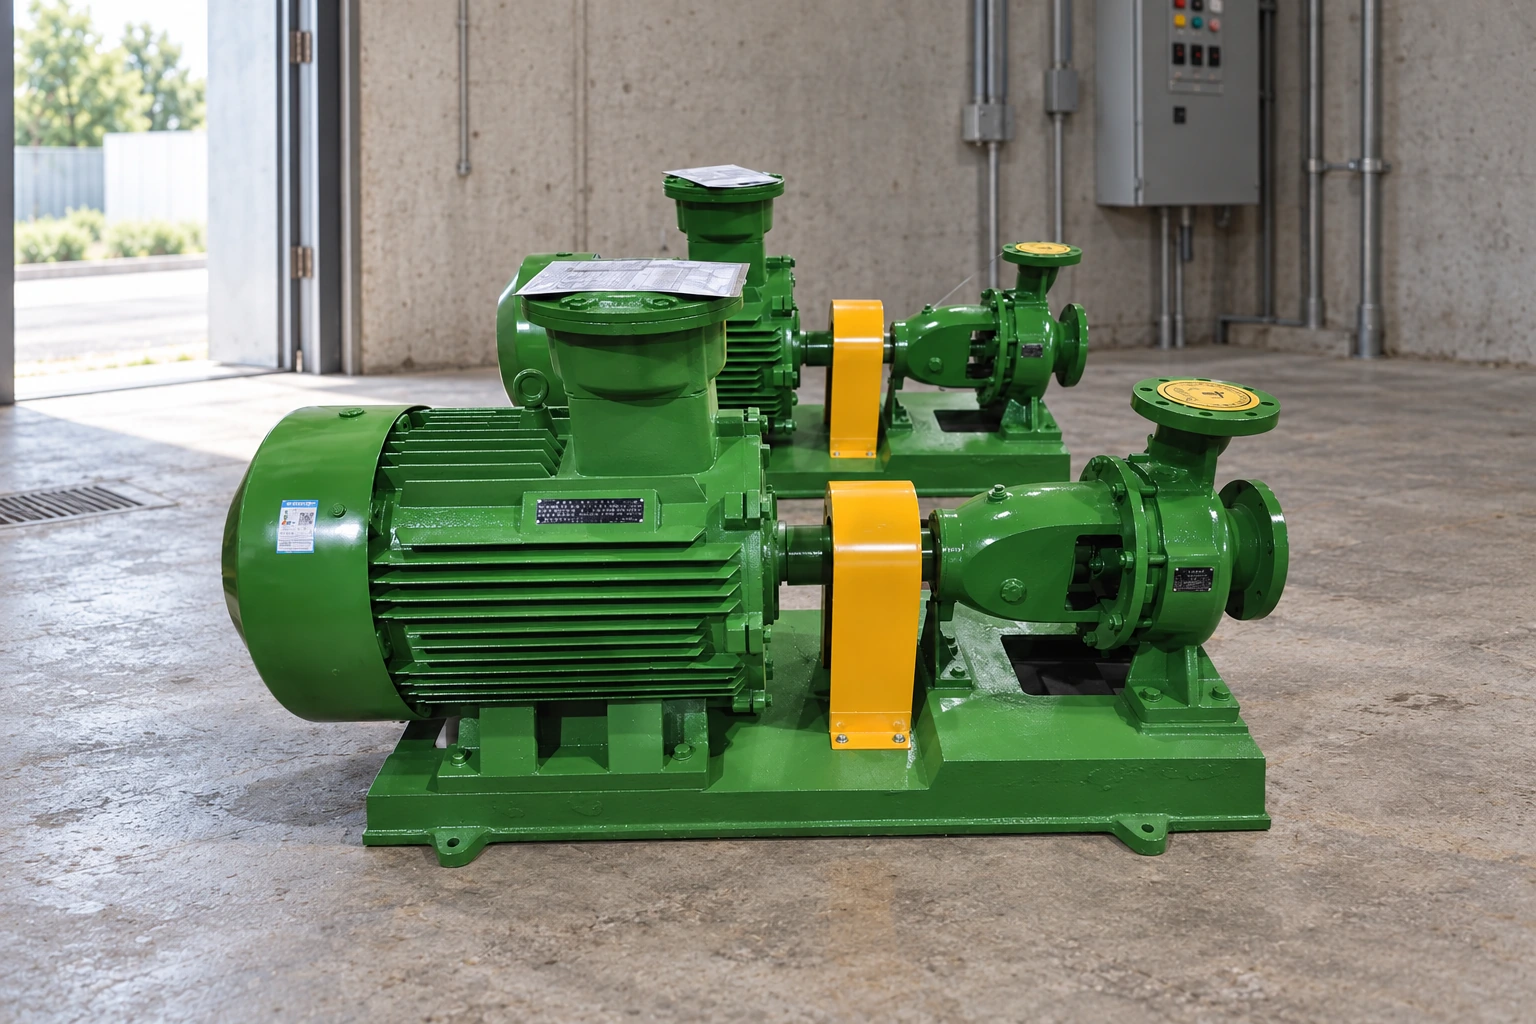
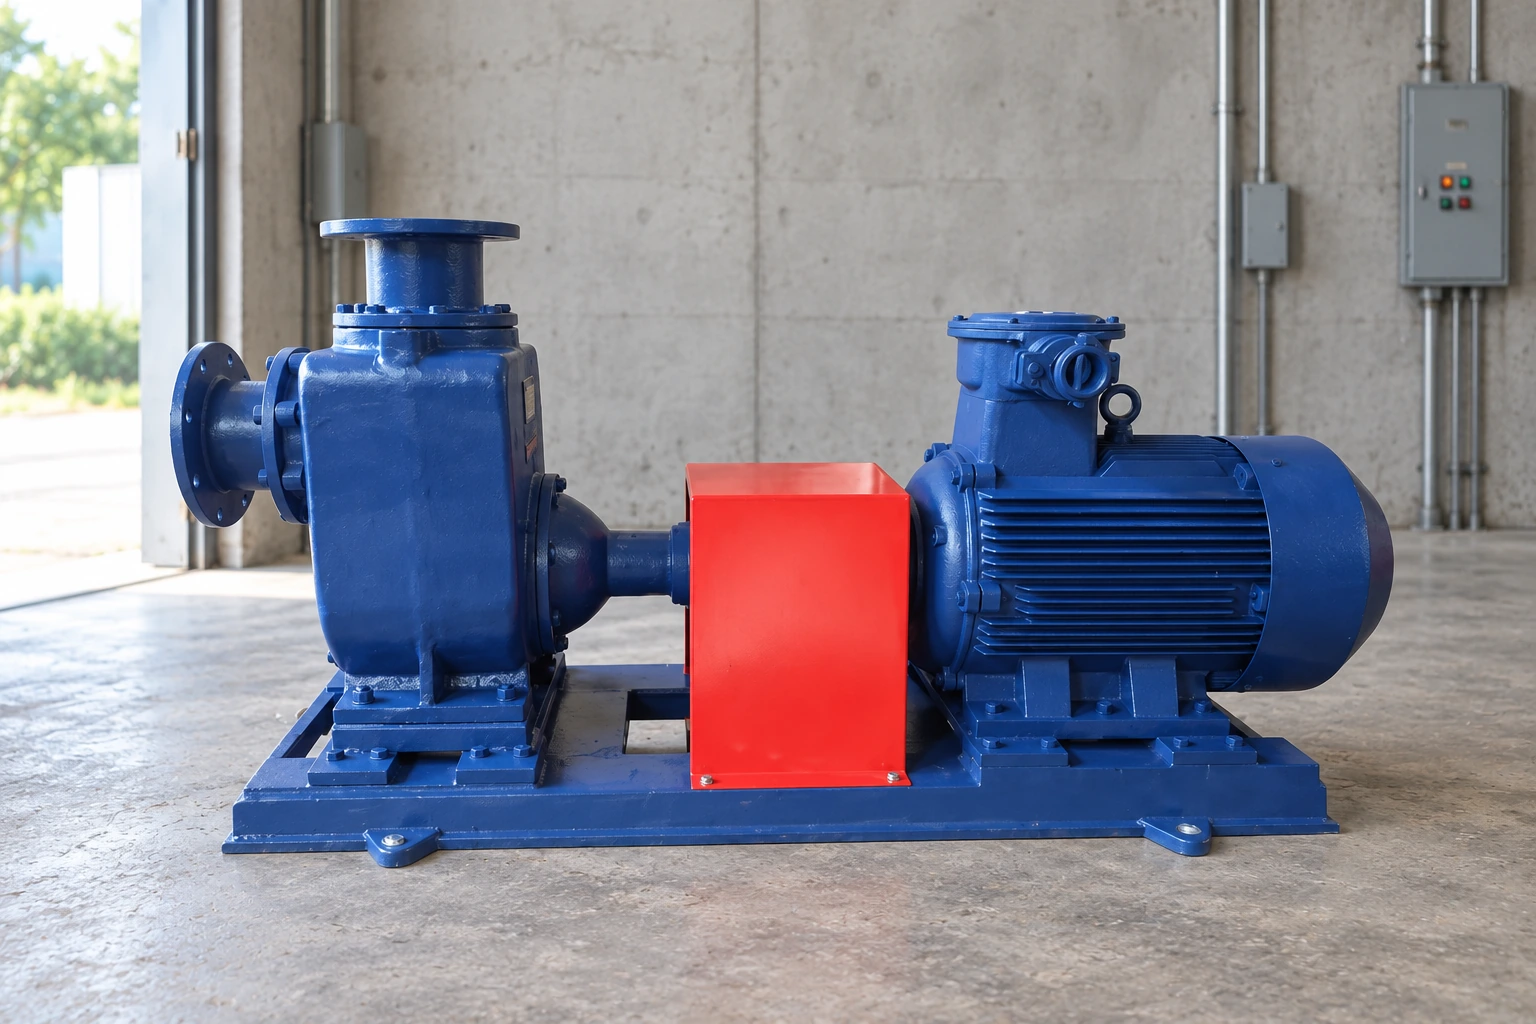
For an inquiry involving the IS-Kreiselpumpenbereich für Reinwasser, provide the individual build information rather than assuming a common register design across the range. Include the parts map, relevant drawing, measured male and female features, setup photographs and proposed disposition. Add the evidence to the Wartungsinspektionsbericht so assembly, repair and purchasing teams use the same record.
Weiterführendes Lernen: Passungen und Toleranzen
The IIT Kanpur NPTEL lecture below introduces engineering fits and tolerances. It helps explain why dimensions need defined limits and matching features. It does not supply the datums, allowable fit or geometric acceptance requirements for a particular pump register.
Häufig gestellte Fragen
Is a casing register the same as the gasket face?
Nein. Ein Register positioniert die Gegenkomponenten, während eine nahegelegene Fläche eine Abdichtung oder axiale Lage bieten kann. Identifizieren und inspizieren Sie die Funktionen separat auf der tatsächlichen Zeichnung.
Besteht eine Verbindung, die verschraubt wird, die Inspektion?
Nein. Verschraubungen können Störungen verbergen oder eine falsch positionierte Montage ermöglichen, um zu schließen. Überprüfen Sie die angegebenen Passungsmaße und geometrischen Beziehungen vor der Freigabe.
Is measuring the register diameter enough?
Nicht immer. Die Inspektion kann auch den passenden Durchmesser und die Beziehung zu einem vorgegebenen Bohrung, einer Fläche oder einer Mittellinie erfordern. Verwenden Sie die definierten Bezugspunkte und Methoden des Geräts.
Can coupling alignment correct a damaged register?
Sie stellt die Lagefläche oder deren Geometrie nicht wieder her. Lösen Sie die Anforderungen an die interne Montage separat, bevor Sie das entsprechende externe Ausrichtungsverfahren abschließen.
What should accompany a repair request?
Geben Sie die Geräteidentifikation, Referenzen zu den Gegenstücken, die Ausrichtung, Fotos, einzelne Messwerte, Angaben zu den Messgeräten und zum Prüfaufbau, Abnahmekriterien sowie den vorgeschlagenen Reparaturumfang an.