Pump bearing spacer inspection checks the component that establishes a defined separation or contact relationship within a bearing assembly. Confirm the spacer’s location and orientation, inspect its bore and end faces, and compare the required dimensions with the controlled drawing. A sleeve that slides onto the shaft is not automatically the correct bearing spacer. This guide concerns internal bearing-stack components, rather than a removable coupling spacer or a shaft-protection sleeve. It does not provide a universal spacer length, endplay value or preload adjustment method. The actual pump construction and assembly instructions govern every acceptance and repair decision.
Establish the spacer’s function from the section drawing
Begin with the equipment serial number, shaft reference, bearing arrangement and current drawing revision. Identify which parts contact each spacer face and how the spacer fits into the assembly sequence. Similar cylindrical parts can perform different functions, so distinguish a bearing spacer from a seal sleeve, coupling component or loose handling aid.
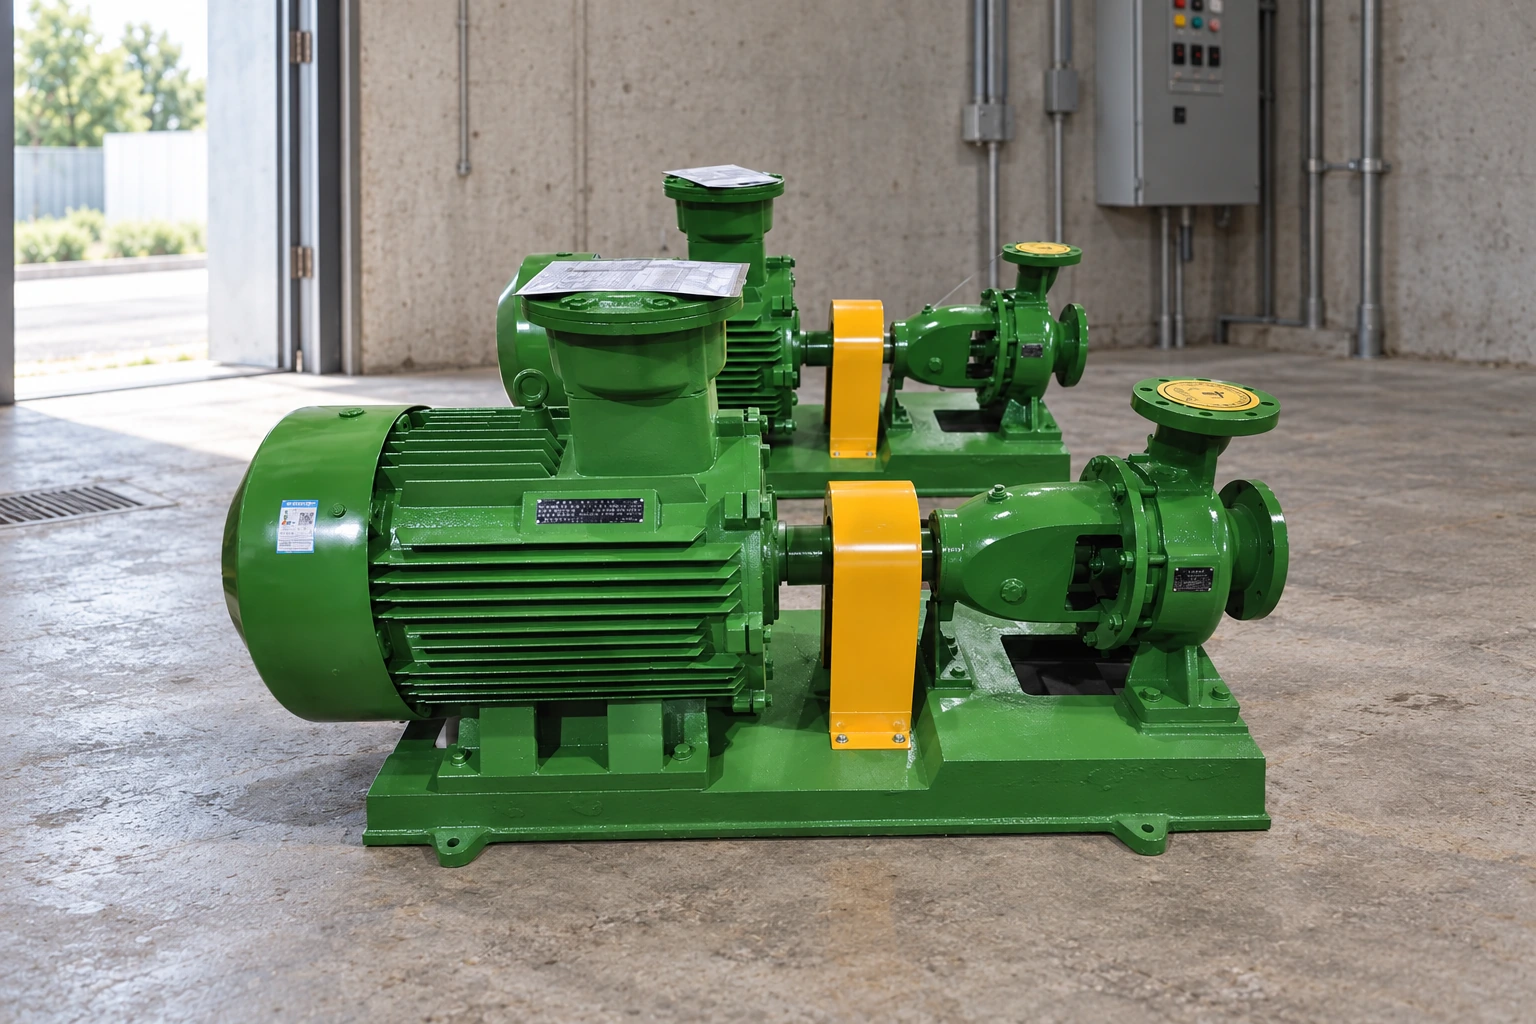
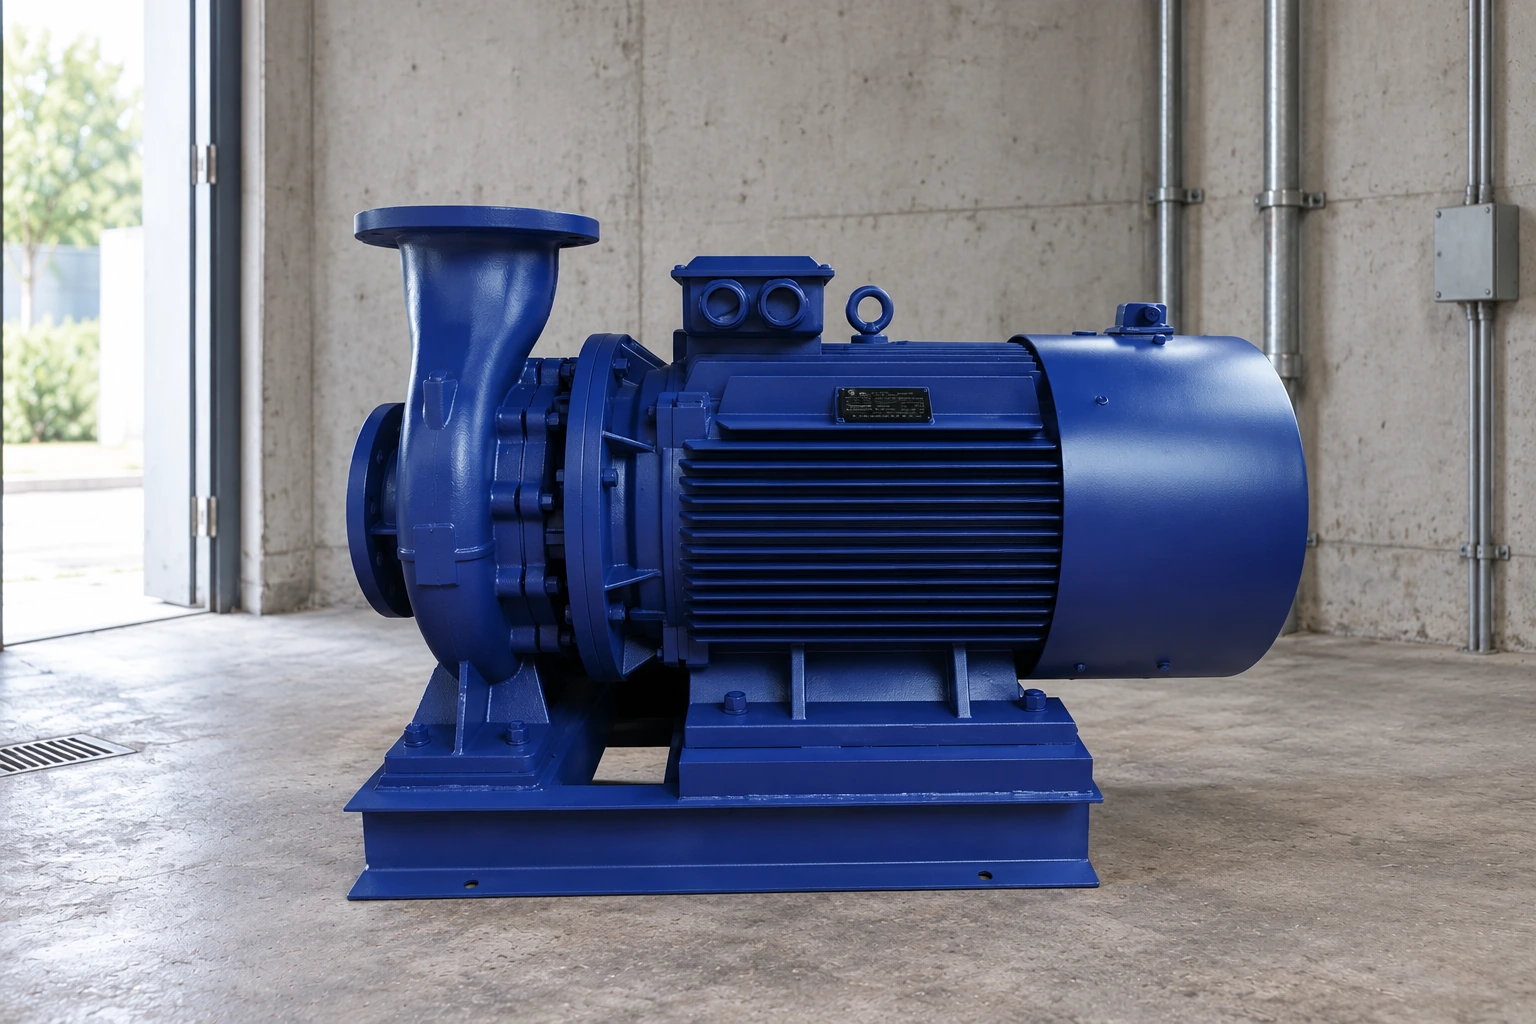
Record any orientation features, relieved corners, steps or unequal ends shown by the drawing. Do not infer interchangeability from outside diameter alone. If a pump has been modified, establish whether the bearing or spacer specification changed with it. The public IS clean-water centrifugal pump page helps identify a relevant equipment family but does not reveal the serial-specific internal bearing stack. Obtain the actual section and parts information before treating a catalogue image or a removed sleeve as evidence of the intended spacer arrangement.
Preserve order and orientation during dismantling
Photograph the assembly before separating parts and create a simple component map. Label the spacer and its adjacent components using a method that will not damage functional surfaces. Keep removed spacers grouped with the correct shaft and bearing position. Mixing parts from two similar pumps can produce a convincing-looking assembly with the wrong axial relationship.
Use the site isolation and safe dismantling plan. The Guidance de maintenance HSE provides general UK context for controlling maintenance hazards, not a bearing-stack disassembly method. Record any difficulty in removal, unexpected gap, looseness or evidence of contact. If a spacer is damaged during dismantling, distinguish that event from its as-found condition. Preserving this sequence is especially important where the workshop receives individual components rather than the assembled rotor and cannot reconstruct the original arrangement independently.
Clean the component without altering its faces
Remove deposits using a process compatible with the material and inspection objective. Expose the end faces, bore, outside surface and any reliefs. Avoid uncontrolled abrasive cleaning that changes length, rounds edges or removes evidence of uneven contact. Photograph suspect areas before and after cleaning and record the method used.
Look for corrosion, fretting, cracks, dents, burrs and displaced metal. Note whether damage is concentrated on one face, around a corner or along the bore. A polished surface does not prove the spacer has the correct geometry. Do not stone or grind the ends simply to obtain an attractive contact pattern before establishing acceptance requirements. If a flaw needs additional examination, define that examination through a qualified person. Keep the component held until its condition is understood rather than allowing cleaning to become an undocumented dimensional repair.
Inspect each contact face and its mating surface
Identify the actual mating components and examine their contact surfaces along with the spacer. Record uneven witness marks, local impact, corrosion and signs that contact occurred where the drawing does not intend it. Check corner relief and any orientation requirement against the correct component references.
Le Document d'inspection de la pompe OISD includes general checks of sleeve and rotating-component condition. It supports inspecting related parts together, but it does not establish a spacer specification for an individual BORRAPUMP assembly. Use the pump drawing and approved procedure to determine what matters for this job. Replacing the spacer alone may leave damage on a shaft shoulder or bearing face unresolved. Equally, accepting adjacent parts does not automatically accept the spacer. Record the interfaces explicitly so the release decision covers the intended assembly rather than a collection of separately cleaned components.
| Feature | Inspection record | Equipment-specific requirement |
|---|---|---|
| Identity and orientation | Part reference, location and end markings | Correct component and assembly direction |
| End faces | Damage, contact evidence and measurements | Required length and face geometry |
| Bore | Surface condition and defined measurements | Specified relationship to shaft |
| Reliefs and steps | Shape, condition and matching component | Clearance and seating requirements |
| Complete stack | Actual component order and final checks | Accepted assembled relationship |
This table is a qualitative planning tool. It provides no universal tolerance or authority to adjust a bearing setting.
Measure the specified features with a defined method
Select instruments and a setup suitable for the drawing requirements. Record calibration status, preparation, measuring positions and the relevant datums. If length must be checked at multiple locations to assess the face relationship, retain the individual readings instead of reporting only an average that hides variation. Use the specified method for any geometric requirement beyond simple length.
Take care to distinguish nominal size, a measured worn size and an accepted drawing dimension. A caliper reading on an unclean or damaged face may be useful for preliminary identification without being adequate for final release. State that distinction. The guide d’inspection de l’ajustement des roulements addresses the related shaft and housing interfaces. Do not interpret a suitable bore fit as proof that the spacer length or end-face relationship is acceptable. Each feature needs the examination appropriate to its function.
Check the complete stack before changing a dimension
A suspected spacer problem may involve the wrong bearing reference, a missing part, an incorrect orientation or damage elsewhere in the assembly. Compare the actual component order with the approved section. Confirm that the bearing arrangement and retaining components are the correct versions before proposing a shorter or longer spacer.
Do not machine the spacer until an assembled reading looks familiar without first understanding the design. Changing length can alter the relationship of adjacent components. An approved repair or modification should state the intended finished dimensions, associated checks and any revised part identification. If several components have been replaced, preserve the old references and explain the changes. A future maintenance team needs to know whether it is looking at an original assembly or a documented modified stack; otherwise, a replacement ordered to an old drawing may no longer match the installed arrangement.
Resolve surface damage and reuse decisions
Classify the spacer as accepted against a named requirement, replaced or held for engineering review. Record the observations and measurements supporting the decision. A small-looking burr can matter to seating, while a dramatic stain may be removable deposit; neither appearance alone establishes the final disposition. Use the approved inspection and repair requirements.
If refinishing is authorized, retain pre-repair evidence and verify the final dimensions and geometry. Do not compensate for uncontrolled face removal with a loose shim unless an approved design calls for it. Inspect any affected mating part before releasing the repaired spacer. The separate shaft shoulder inspection guide addresses the abutment side of this relationship.
Order replacements with the assembly information
A useful inquiry includes the pump serial number, spacer part reference, section drawing, bearing references, measured condition and previous repair history. State the material and finish requirements where the controlled documents provide them. Mark unknown information rather than guessing from colour, weight or a worn sample.
A replacement copied solely from a damaged part can reproduce an incorrect dimension or miss a relief that appears unimportant. Ask the supplier to resolve uncertainty against the assembly. The pump spare-parts identification guide explains how to separate confirmed references from workshop estimates. Keep any approved substitution linked to the work order and update the component identity accordingly. This prevents the purchasing record from describing a generic sleeve when the delivered part actually carries a specific bearing-stack function and revised dimensional requirement.
Verify assembly and document release
Assemble accepted components in the specified order and orientation using suitable tooling. Confirm clean mating surfaces and account for temporary protection materials. Perform the seating, retention and associated assembly measurements required by the procedure. Do not use rotation by hand or nut tightening effort as a substitute for those checks.
Attach the component map, photographs, individual measurement results, repair approvals and final assembly record to the rapport d'inspection de maintenance. State the method and limitations of each check. A release note should show which spacer was installed and why it was accepted, rather than simply saying the bearing assembly was rebuilt. Retain unresolved findings as explicit holds. This gives the operator, repair contractor and future maintenance team a consistent record of the actual assembly condition and the instruction that governed its return to service.
Further learning: reading fits and tolerances
The IIT Kanpur NPTEL lesson below explains dimensional limits and fits. It provides useful background for interpreting spacer and shaft drawings. It is not a pump bearing adjustment procedure and does not establish a spacer length or permissible face error. Apply the equipment-specific section and inspection requirements.
Foire aux questions
Un espacement de roulement est-il identique à un espacement de coupleur ?
No. They serve different assembly locations and functions. Identify the component from the section drawing and parts list rather than using the word spacer as evidence that two parts are interchangeable.
Une entretoise peut-elle être acceptée parce qu'elle glisse sur l'arbre ?
Cette observation ne permet pas d'établir son identité, sa longueur, la géométrie de la face ou la relation finale de l'empilement. Inspectez les caractéristiques spécifiées et vérifiez l'assemblage complet selon la procédure de l'équipement.
Les deux extrémités doivent-elles être usinées pour éliminer les dommages ?
Seul une réparation approuvée peut autoriser des modifications dimensionnelles. Enregistrez l'état d'origine et définissez les exigences d'acceptation finale avant de retirer du matériau d'une face qui contrôle une relation d'assemblage.
Un cales peut-il compenser un espaceur incorrect ?
Ne pas improviser une compensation. Déterminez pourquoi l'assemblage est incorrect et obtenez une décision d'ingénierie documentée concernant l'entretoise, les composants en contact et les vérifications finales requises.
Que doit être enregistré après le remontage ?
Enregistrez l'identité de la pièce installée, la commande, l'orientation, les mesures acceptées et les vérifications nécessaires pour l'assise ou la retenue. Liez toute réparation ou substitution à son approbation et incluez la personne responsable de la libération.